Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Certified high-density industrial pallet racks engineered for UK cold storage, controlled ambient distribution hubs, and automated pharmaceutical supply chains.
High-density double-reach storage maximizing UK pharmaceutical warehouse volumetric footprint. Configured with specialized pantograph reach trucks for dual-pallet row access.
Request UK Project Quote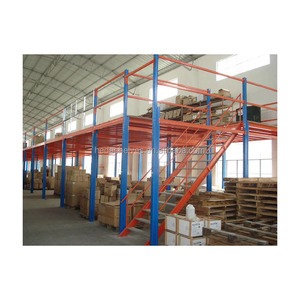
Engineered steel mezzanine floors doubling floor space for UK NHS supply hubs, batch-picking operations, and pharmaceutical packaging cleanroom staging environments.
Request Technical Specs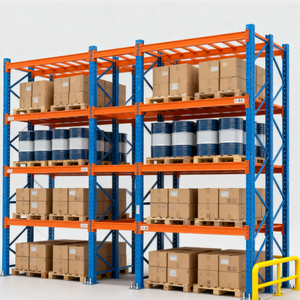
Reinforced upright columns engineered to BS EN 15512 specifications. Features high-tensile steel cold-rolled profiles for heavy payload security in bulk pharmaceutical hubs.
Request CAD Layout Design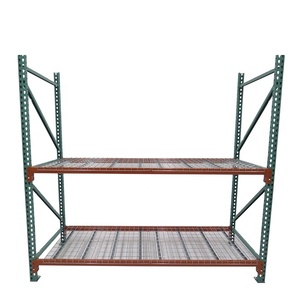
Interchangeable teardrop and box-beam structural configurations. Anti-microbial polyester powder coating specifically formulated for UK hygienic storage audits.
Inquire Direct Pricing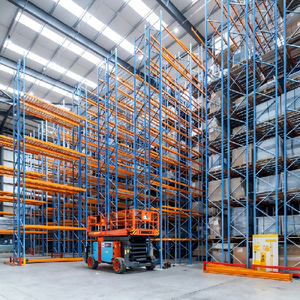
Fine-tuned vertical shelf adjustment in 75mm increments. Optimized for automated high-bay warehouses demanding precise millimeter-level beam adjustments for pallet overhang.
Consult Technical Engineer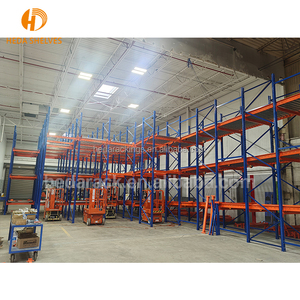
First-In, First-Out dynamic roller system ensuring strict batch control and FEFO (First-Expired, First-Out) compliance for temperature-sensitive drugs and active ingredients.
Request Flow Rate Specs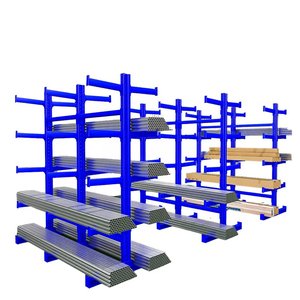
Unobstructed front-access storage for long pipes, stainless steel process tubes, packaging rolls, and liquid storage drums utilized in UK pharmaceutical synthesis facilities.
Get Cantilever Estimate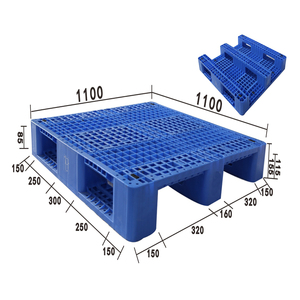
Designed specifically to interface with 4-way entry plastic hygiene pallets and Euro-pallets (1200x800mm / 1200x1000mm) without beam deflection or floor contamination.
Download Compatibility GuideThe United Kingdom's pharmaceutical supply chain operates under some of the most rigorous regulatory scrutiny in the world. Enforced by the Medicines and Healthcare products Regulatory Agency (MHRA) under Good Distribution Practice (GDP) guidelines (the "Orange Guide"), warehouse storage infrastructure is no longer viewed merely as structural static steel—it is an integral component of cold-chain integrity, batch traceability, contamination prevention, and structural safety.
As a specialized B2B manufacturer and exporter of high-density warehouse racking systems for the UK, our structural designs directly address the thermodynamic and micro-environmental challenges of pharmaceutical storage. Standard commercial warehouse racking frequently fails UK MHRA inspections due to substandard surface coatings that shed particles, inadequate perimeter airflow clearance, rust susceptibility under high relative humidity, or structural steel embrittlement in sub-zero freezer hubs.
Critical MHRA Compliance Note: Section 3.2 of UK GDP guidelines mandates that pharmaceutical products must be stored off the floor with minimum 100mm clearance from walls and structural beams to facilitate continuous thermal circulation, pest control monitoring, and automated wash-downs. Our custom racking profiles feature engineered offset footplates and integrated wire mesh decking to exceed these requirements.
Our pharmaceutical racking systems utilize premium-grade cold-rolled structural steel (Q235B & Q355B equivalent to S235JR and S355JR under BS EN 10025 standards). Every upright frame and load beam undergoes automated ultrasonic flaw testing, shot-blasting to Sa 2.5 cleanliness, and electrostatic application of non-porous, anti-bacterial epoxy-polyester powder coats (tested against ISO 22196 for microbial resistance). For cleanrooms and wet-wash processing staging areas, hot-dip galvanizing to BS EN ISO 1461 guarantees non-corrosive performance over a 25-year service life.
Detailed performance benchmarks comparing standard logistics racking vs. specialized UK pharmaceutical-grade structural systems exported by our manufacturing plant:
| Engineering Specification | Standard Commercial Pallet Rack | UK Pharma-Grade Racking (Our Plant Specs) | Regulatory / Structural Relevance |
|---|---|---|---|
| Steel Material Grade | Standard Mild Steel (Q235) | High-Tensile Cold-Rolled Q355B / S355 Structural Steel | BS EN 15512 Structural Safety Code |
| Surface Coating Technology | Standard Industrial Paint / Powder Coating | Anti-Bacterial Non-Porous Epoxy Powder Coating (ISO 22196) | MHRA GDP Hygiene & Contamination Prevention |
| Cold-Store Performance (-30°C) | Risk of Ductile-to-Brittle Transition Failure | Charpy V-Notch Impact Tested Structural Alloys & HDG Finish | Cold-Chain Vaccine & Biologics Storage Integrity |
| Perimeter Airflow Engineering | Flush Floor Mounting (Restricted Flow) | Custom Offset Anchor Plates & Open-Deck Wire Mesh | Eliminates Thermal Stagnation & Hot Spots |
| Structural Load Safety Factor | 1.40 - 1.50 | 1.65 (Exceeds SEMA & FEM 10.2.02 Standards) | BS EN 15635 Inspection & Maintenance Protocol |
Tailor-made racking topologies designed for the specific geographic hubs, architectural floorplans, and regulatory demands of the UK life sciences sector.
In strategic distribution hubs like Daventry, Rugby, Northampton, and Magna Park, 3PL providers manage massive cold-chain operations (+2°C to +8°C and -25°C deep freeze). Our Gravity Pallet Flow (FIFO) and Double Deep Racking systems maximize floor area utilization while maintaining continuous batch rotation. Hot-dip galvanized uprights resist condensation-induced oxidation, ensuring seamless automated operations for temperature-critical biologics.
NHS regional supply chains require high-throughput multi-tier mezzanine platforms and VNA (Very Narrow Aisle) pallet racking to store hundreds of thousands of medical consumables, diagnostic kits, and prescription medications. Our systems incorporate wire mesh decking, heavy-duty column protectors, and clear weight loading signage compliant with Health and Safety Executive (HSE) HSG76 guidelines.
Within high-tech life science parks across Cambridge, Oxford, and Stevenage, sterile cleanroom staging zones require non-shedding, corrosion-resistant storage. We engineer custom Grade 304 and 316 stainless steel shelving along with specialized smooth-profile powder-coated cantilever racks that eliminate dust-trapping crevices and allow 100% steam or chemical disinfectant wipe-downs.
The UK North West pharmaceutical cluster (Liverpool and Manchester region) relies on high-speed order fulfillment. Our automated VNA pallet racking integrated with guided AGVs (Automated Guided Vehicles) delivers maximum vertical height utilization (up to 15 meters) while achieving sub-millimeter beam deflection tolerances necessary for high-speed robotic picking.
Key operational shifts shaping how UK pharmaceutical supply chain directors, warehouse managers, and procurement leads source racking systems.
UK pharmaceutical companies are under strict NHS Supplier Roadmap requirements to achieve Net-Zero greenhouse gas emissions. As a direct exporter, our manufacturing facility utilizes energy-efficient continuous roll-forming lines, recycled steel scrap recovery, and eco-friendly powder coating formulations that provide full environmental product declarations (EPDs) to support our UK clients' ESG audits.
Following the transition from CE marking to UKCA (UK Conformity Assessed) standards, UK procurement officers require full structural calculation documentation backed by independent laboratory testing. All our exported structural pallet racking frames comply with UK structural Eurocodes (BS EN 1993-1-1) and carry complete material test certificates (MTC Type 3.1) for frictionless UK building control approval.
Labor availability constraints across UK warehousing hubs have accelerated the adoption of automated pallet flow lanes and shuttle systems. UK operators demand FIFO/FEFO dynamic storage to prevent drug expiry losses. Our dynamic gravity roller tracks feature magnetic speed controllers and drop-out safety stops engineered specifically for delicate liquid medicine totes and glass vials.
With over two decades of dedicated manufacturing excellence in heavy-duty material handling and warehouse racking, Rack Pricing Storage Solutions Co., Ltd. operates as a direct manufacturer and global supplier. We remove intermediary distributor markups while providing end-to-end structural engineering support tailored to UK building codes and MHRA requirements.
From raw steel coil slitting, multi-station automated roll-forming, and robotic welding to our 150-meter automated powder coating line, every manufacturing step is conducted under ISO 9001:2015 quality management systems. We guarantee dimensional tolerances within ±0.5mm on upright profiles.
Our in-house structural engineers utilize AutoCAD and Revit BIM software to convert your warehouse floor plan, floor slab loading limits (kN/m²), and forklift turning radii into fully optimized 2D/3D racking layouts—delivered free of charge within 24 to 48 hours.
Racking components are bundled with steel strapping, wrapped in protective plastic film, and equipped with corner protection boards. Every bundle is clear-labeled with part numbers and structural assembly tags to ensure rapid customs clearance and efficient unloading at major UK ports including Felixstowe, London Gateway, Southampton, and Liverpool.
Our structural calculations align with SEMA (Storage Equipment Manufacturers Association) Code of Practice and BS EN 15635 requirements. We supply complete load notices, safety pin locking mechanisms, and heavy-duty floor anchor bolts with every export container.
Expert technical answers regarding UK structural compliance, shipping lead times, surface finishes, and MHRA warehouse inspections.
Our pharmaceutical racking systems are specifically engineered to pass MHRA inspections. We design the floor layout to ensure a minimum 100mm wall and perimeter clearance for air circulation and pest control inspection. Furthermore, our anti-bacterial non-porous powder coating prevents dust build-up and withstands chemical sanitization. Open-deck wire mesh decking options also eliminate dust traps while ensuring sprinkler water penetration compliant with UK Fire Safety Regulations.
Yes. All structural calculations, cold-rolled steel section properties, and load-bearing capacities are engineered in accordance with BS EN 15512 (Steel static storage systems - Adjustable pallet racking systems) and align with SEMA guidelines. We supply official safe working load (SWL) notices to be affixed to beam ends, which satisfies UK Health and Safety Executive (HSE) inspectors during annual BS EN 15635 racking safety audits.
For deep sub-zero cold stores and high-humidity vaccine cold rooms, we recommend either our specialized low-temperature flexible epoxy powder coat or Hot-Dip Galvanized (HDG) steel finished according to BS EN ISO 1461. Standard industrial paint can micro-crack and flake under severe thermal contraction; our cold-store coatings maintain structural adhesion and prevent micro-corrosion down to -30°C.
Production lead time at our factory typically ranges from 14 to 21 days depending on total tonnage and custom color requirements (RAL spectrum). Direct sea freight shipping from our port to major UK ports (Felixstowe, Southampton, London Gateway, Liverpool) usually takes between 26 to 32 days. In total, UK buyers can expect door-to-port delivery within 6 to 7 weeks from final CAD approval.
Yes. We regularly produce compatible upright profiles, beam connections, and accessories designed to match major European and UK racking profiles (including 75mm pitch profiles). Simply provide our engineering team with your current upright dimensions, hole pitch measurements, and beam connector photographs, and we will manufacture precision-matched extension bays or replacement components.
Connect directly with our senior structural engineers and B2B export team. Receive free CAD warehouse drawings, structural load calculations, and factory-direct FOB/CIF UK pricing within 24 hours.
Contact Us