
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Engineered for maximum load structural integrity, seamless automation interface, and rigorous ISO/EN compliance.
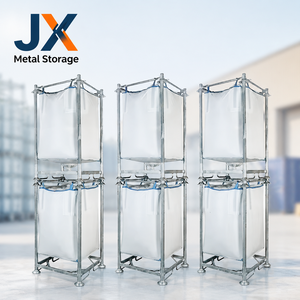
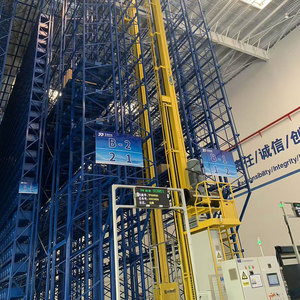
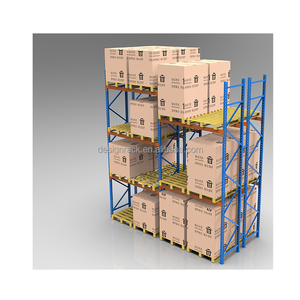
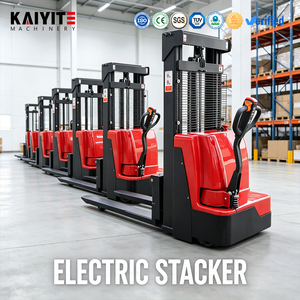
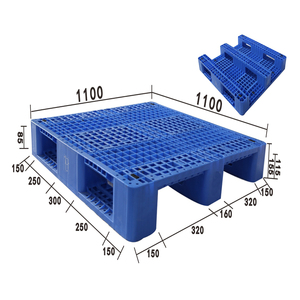
In modern high-throughput fulfillment centers, automotive manufacturing plants, and cold-chain distribution hubs, the synergy between structural pallet storage racks and dynamic conveyor transport systems defines operational velocity. As a premier **China Pallet Conveyor Storage System Manufacturer & Factory**, Rack Pricing Storage Solutions Co., Ltd. delivers custom-engineered material handling frameworks designed to withstand heavy unit loads (up to 3,000 kg per position) while integrating seamlessly with automated guided vehicles (AGVs), Autonomous Mobile Robots (AMRs), and AS/RS stacker cranes.
Optimal material transport requires rigorous physical modeling: load-deflection ratios under EN 15512 standards, structural torsional rigidity under dynamic start-stop momentum, and precision roller surface tolerances. By combining cold-rolled high-tensile steel structural profiles (Q235B & Q355B grades) with smart Motor-Driven Roller (MDR) technology, our conveying storage platforms maximize vertical cube utilization while reducing operational bottlenecking.
Comparative technical performance metrics to guide industrial engineers and warehouse architects in selecting optimal handling equipment.
| Conveyor / Rack Sub-System | Load Capacity (KG/Unit) | Max Speed / Throughput | Structural Material Grade | PLC / WCS Integration | Primary Application Field |
|---|---|---|---|---|---|
| Heavy-Duty Heavy Roller Conveyor | 500 - 2,500 kg/m | 18 - 30 m/min | Precision Steel Tube / Q235B Frame | Siemens S7-1500 / Profinet | Main pallet transport, Inbound/Outbound staging |
| Multi-Strand Heavy Chain Conveyor | 1,000 - 3,000 kg/pallet | 12 - 20 m/min | Forged Alloy Chain / C-Channel Frame | EtherNet/IP / Modbus | Cross-conveyance, 90-degree transfers, plastic/wooden pallets |
| AS/RS Curved Stacker Crane Racking | Up to 1,500 kg/bay | Horizontal speed: 200m/min | High-Tensile Cold Rolled Q355B Steel | Fully Automated WCS/WMS | High-density dark warehouses, pharmaceutical & cold storage |
| Gravity Pallet Flow Racking | 800 - 1,500 kg/position | Controlled speed: 0.3 m/s | Structural Steel Frame & Brake Rollers | Passive Mechanical Safety | FIFO (First-In, First-Out) high-density buffer storage |
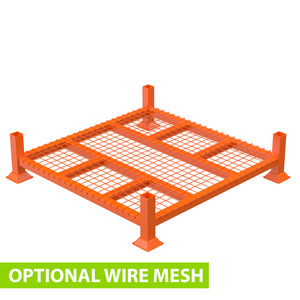
| Post Pallet Stacking Frame (Detachable) | 1,000 - 2,000 kg static | N/A (Forklift / Stacker load) | Hot-Dip Galvanized / Powder Coated Steel | Manual / Modular Stack | Bulk bag storage, seasonal overflow inventory, shipping stay |
Modular component design allows enterprise buyers to scale handling throughput with minimal mechanical reconfiguration.
Utilizing 24V/48V low-voltage DC brushless motor rollers paired with internal planetary gearboxes, our MDR systems provide precise Zero-Pressure Accumulation (ZPA). Energy consumption drops by up to 60% compared to continuous-running traditional drive lines while eliminating dynamic backpressure during pallet line buffering.
Designed for automated storage and retrieval systems (AS/RS), our racking frameworks feature high-precision guide rails with floor-anchored tolerance plates. Accommodating both single-deep and double-deep stacker crane forks, they ensure sub-millimeter positional alignment at elevation heights reaching up to 40 meters.
Smooth direction changes without pallet orientation shifting. Pneumatically or electrically actuated pop-up chain transfers integrated directly into live roller beds ensure seamless 90-degree branch routing for automated sorting lines without dynamic load destabilization.
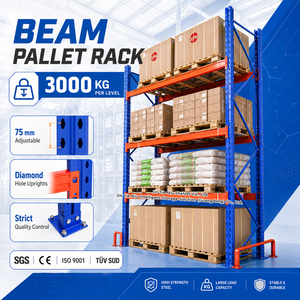
For flexible storage buffers, our cold-rolled steel heavy-duty racking systems feature 50mm/75mm adjustable beam pitches equipped with safety locking pins. Hot-dip galvanized post pallets allow portable vertical stacking (4-6 high) without permanent floor anchor requirements.
Gravity-driven lane storage utilizing precision steel rollers and dynamic magnetic speed controllers. Integrated centrifugal safety brakes prevent runaway acceleration, guaranteeing safe, continuous FIFO movement across deep-lane pallet racks up to 16 pallets deep.
Pre-engineered PLC control cabinets with integrated Ethernet switches, safety relays, and barcode scanning sensor brackets. Fully compatible with enterprise SAP, Oracle, and Manhattan WMS for real-time inventory tracking, sensor diagnostics, and predictive maintenance monitoring.
Strategic technology developments reshaping global supply chain investments, warehouse automation economics, and procurement strategies.
Procurement teams are shifting away from centralized AC motor chain networks toward distributed 48V DC Motor Driven Roller (MDR) architectures. The higher voltage profile reduces wiring copper gauge, slashes thermal heat generation in refrigerated warehouses, and allows individual roller zone diagnostics via IO-Link smart sensors.
Modern distribution facilities are removing static perimeter conveyors in favor of mobile AMR fleets interlocked with fixed pallet conveyor pick/drop nodes. This requires pallet conveyor manufacturers to engineer tight-tolerance auto-docking alignment frames equipped with infrared optical communication eyes for dynamic handshakes.
Industrial B2B buyers now mandate vibration, temperature, and current sensors embedded into conveyor drive bearings and AS/RS stacker crane tracks. Cloud analytics detect early bearing fatigue or rack column micro-deflections before mechanical failure occurs, boosting total operational availability past 99.9%.
With global cold chain logistics expanding rapidly, dynamic racking and conveying components must operate reliably at -30°C without lubrication freezing or synthetic polyurethane roller shedding. Specialized cold-grade steel alloys and synthetic arctic greases are becoming mandatory buyer specifications.
Combining 20+ years of structural steel fabrication with end-to-end quality controls for international engineering contractors.
Our 50,000 sqm manufacturing base houses 16 continuous automated roll-forming lines, 3D laser tube cutters, and robotic welding stations. We maintain strict geometric dimensional tolerances (±0.5mm) across 12-meter upright profiles and conveyor frame channels.
Features an advanced Swiss Gema fully automated electrostatic powder coating line. Components undergo 6-stage chemical pre-treatment (degreasing, phosphating, pure water rinsing) guaranteeing superior salt-spray corrosion resistance (500+ hours) and impact durability.
We don't just sell hardware—our experienced logistics software engineers provide free CAD layout design, structural finite element analysis (FEA), and BIM 3D models to ensure seamless structural integration with your building slab and HVAC systems.
Components are modularly packaged with edge protectors, waterproof plastic wrapping, and steel strap tie-downs. Custom container loading schemes maximize volume fill rates (up to 98% space utilization), significantly reducing ocean freight cost per pallet position.
Expert technical answers covering custom engineering, international safety compliance, and OEM factory lead times.
To deliver a precise technical proposal and CAD layout, our engineering team requires: (1) Warehouse building dimensions and clear height under roof trusses; (2) Pallet specifications including width, depth, height, and maximum unit weight; (3) Pallet bottom runner configuration (e.g., 3-runner, 9-leg, plastic or wooden); (4) Required system throughput (pallets per hour); and (5) Operating environment conditions (ambient, cold storage, cleanroom).
Yes. Our automated pallet conveyor systems utilize industry-standard PLC controllers (Siemens, Allen-Bradley, Schneider) and support Profinet, EtherNet/IP, and Modbus TCP protocols. This allows effortless software handshakes with third-party Warehouse Management Systems (WMS) and Warehouse Control Systems (WCS).
Our heavy-duty racking platforms and conveyor support structures are calculated and tested according to European Standard **EN 15512** (Structural Steel Racking Systems), **EN 15635** (Application and Maintenance of Storage Equipment), and American **RMA MH16.1** specs. Seismic design options up to Zone 4 acceleration are available for high-earthquake regions.
We execute strict ISO 9001:2015 quality control routines. Raw steel coils undergo yield strength testing upon arrival. During production, continuous laser sensors monitor roll-forming wall thickness, ultrasonic weld testing is conducted on beam connectors, and dry film thickness gauges audit powder coating coverage across every batch.
Standard heavy-duty racking orders ship within 15 to 25 days from contract confirmation. Complex automated pallet conveyor lines and custom AS/RS racking frameworks typically require 30 to 45 days, depending on mechanical component integration and electrical cabinet factory acceptance testing (FAT).
Yes. Every shipment includes comprehensive installation manuals, labeled part-numbered assembly drawings, and video guides. For large-scale automation projects, we can dispatch senior installation engineers or offer full remote VR engineering support to assist your local installation team.