Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Engineered for maximum floor space utilization, safety compliance, and seamless forklift integration.
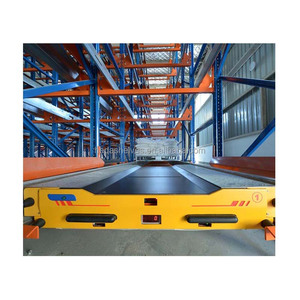
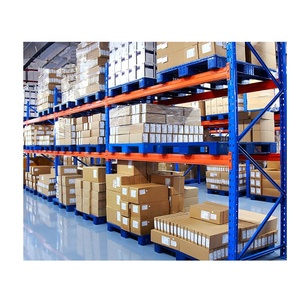
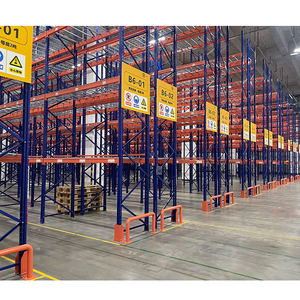
As global supply chains navigate volatile real estate prices and escalating industrial footprint costs, logistical decision-makers must prioritize warehouse volumetric efficiency. Mobile Pallet Racking (MPR)—often referred to as Powered Mobile Racking or Motorized Heavy-Duty Mobile Shelving—represents a paradigm shift from traditional static warehouse geometry. By mounting conventional selective pallet rack uprights onto heavy-duty electronically controlled chassis that travel along embedded floor rails, MPR eliminates the structural requirement for fixed operational aisles. A single dynamic aisle provides 100% direct access to every pallet position while increasing storage density by 80% to 100% within the exact same building envelope.
Information Gain Benchmark: Transitioning from standard selective racking (requiring multiple 3.5m aisles for reach trucks) to a Powered Mobile Racking arrangement reduces total aisle footprint by up to 45%, decreasing cold-storage refrigeration power consumption per pallet by up to 40%.
The structural physics of mobile pallet racking relies on precision cold-rolled structural steel profiles (primarily high-tensile Q235B or Q355B grades), coupled with synchronised electric drive motors. When an operator requests access to a specific rack face—via remote control, integrated warehouse management software (WMS), or an interface panel—the individual rack banks slide laterally with millimeter-level precision. Multi-level safety interlocks, including photoelectric light curtains, physical impact bumpers, and emergency deceleration circuits, guarantee compliance with international safety guidelines such as EN 15635 and OSHA 29 CFR 1910.
An engineering-led evaluation of leading global manufacturers based on structural integrity, automation compatibility, and international export performance.
| Supplier / Exporter | Manufacturing Core | Max Bays Load Capacity | PLC & Automation Integration | Compliance Standards | Export Strengths |
|---|---|---|---|---|---|
| Rack Pricing Storage Solutions | In-house Cold Roll-Forming & Powder Coating | Up to 24,000 kg / Mobile Block | WMS / Radio Shuttle / AMR Sync | EN 15635, FEM 10.2.02, ISO 9001 | Direct Factory Pricing, Free CAD Layouts, Labeled Container Packing |
| SSI Schaefer | Automated System Integration | Up to 20,000 kg / Mobile Block | Proprietary WMS / AGV Interfaces | EN 15635, CE Marking | Global Turnkey Enterprise Projects |
| Stow Group | Heavy Industrial Rack Rolling | Up to 22,000 kg / Mobile Block | RF Control / PLC Smart Hubs | FEM 10.2.02, ISO 14001 | European Distribution & Logistics Hubs |
| Mecalux | Warehouse Software & Steel Racks | Up to 18,000 kg / Mobile Block | Easy WMS Integrated Control | OSHA Compliant, CE Certified | North & South American Logistics Supply |
| Jungheinrich | Material Handling & Racking | Up to 20,000 kg / Mobile Block | Full Fleet Management Sync | EN 15635, ISO 9001 | Intralogistics System Integration |
| Kardex Remstar | Dynamic Automated Storage | Up to 15,000 kg / Mobile Block | Modular Control Systems | CE, ISO 9001 | High-Density Small Item & Light Pallet Modules |
| Dexion Storage Systems | Industrial Pallet Racks | Up to 20,000 kg / Mobile Block | PLC Interlocked Sensor Panels | FEM Standards, AS 4084 | Asia-Pacific & Australasia Operations |
| Montel Systems | High-Density Mobile Storage | Up to 16,000 kg / Mobile Block | SmartTouch Controller Panels | ISO 9001, OSHA | Heavy Duty Industrial & Commercial Modules |
| AR Racking | Structural Steel Forming | Up to 24,000 kg / Mobile Block | Automated Shuttle Compatible | EN 15635, ISO 3834-2 | Customized Structural Engineering & Exporting |
| NEDCON Storage Systems | Custom Warehousing Solutions | Up to 22,000 kg / Mobile Block | Integrated Safety Light Curtains | FEM 10.2.02, CE Compliance | Tailored European Logistics Installations |
Modern powered mobile racks are no longer isolated mechanical assets. Advanced procurement requires PLC platforms that interface natively with Enterprise WMS via API, opening aisles automatically before the forklift operator arrives at the bay entrance to eliminate waiting cycles.
With cold storage operations bearing high electricity tariffs, dense mobile racking configured for sub-zero environments (-30°C) maximizes thermal efficiency by storing more pallets per cubic meter of refrigerated volume.
Next-generation mobile mobile bases incorporate optical LIDAR scanning arrays alongside distance-sensing photo-electric beams. The system creates continuous optical protection zones, halting carriage movement instantly if an unexpected object or person enters an open aisle.
Replacing legacy central shaft drives, direct-drive electric gear motors installed on individual wheel assemblies decrease mechanical wear, lower noise decibels below 65dB, and extend operational lifespans past 15 years with minimal maintenance.
Combining mobile rack bases with automatic radio shuttle runners within multi-deep channels unlocks ultra-dense storage dynamics, allowing fulfillment centers to operate both ultra-compact storage and high-throughput pallet handling simultaneously.
Combining two decades of industrial steel manufacturing with overseas engineering delivery.
Unlike standard trading companies, we manage every phase of racking manufacture within our production plant. From precision profiling of high-tensile steel uprights and beam connectors to automated electrostatic powder coating in customized RAL colors, our end-to-end quality control ensures strict dimensional tolerances and anti-corrosion protection.
No two warehouse spaces have identical floor slab configurations or column layouts. Our structural engineers review your clear height, pallet dimensions, unit weight, and handling equipment specs to provide optimized 2D/3D CAD layout proposals along with certified floor loading calculations—completely free of charge.
Long-distance ocean transport requires structured packing to prevent dynamic transit damage. Every upright bundle, beam pack, and hardware carton is labeled with clear part numbers, edge-protected with heavy-duty cardboard, plastic-wrapped, and loaded into containers according to pre-engineered packing designs to maximize space utilization.
Safety is non-negotiable in heavy material handling. Our systems strictly incorporate safety locking pins, high-impact HDPE upright guards, wire mesh decking, and load capacity signage designed to align with EN 15635, FEM 10.2.02, and OSHA 29 CFR 1910 standards.
Expert answers addressing floor loads, installation precision, emergency power, and maintenance routines.
Consult with our engineering team today to receive a comprehensive CAD layout design, floor slab analysis, and direct factory pricing within 24 hours.
Get Catalog