Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Engineered for extreme structural load-bearing capacity, chemical containment safety, and high-density material handling efficiency.
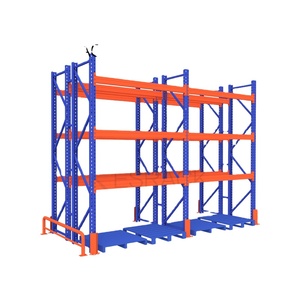
High-load structural beam profile customized for chemical drums, heavy equipment, and bulk palletized stock.
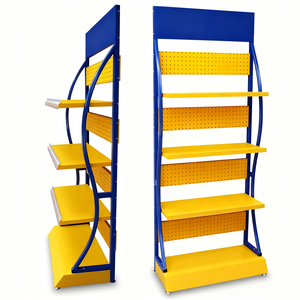
Height-adjustable, high-capacity mobile oil drum racking system featuring lockable industrial casters and anti-roll cradles.
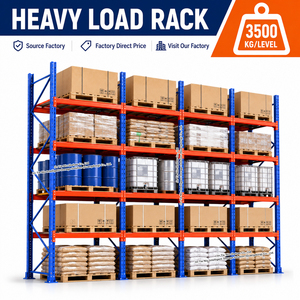
Reinforced structural steel box beams engineered specifically to support up to 3.5 metric tons per shelf level under dynamic conditions.
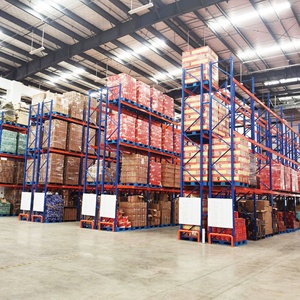
Corrosion-resistant epoxy powder coating optimized for harsh chemical environments and high-frequency forklift handling.
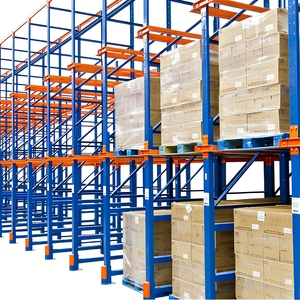
Maximum floor space utilization for bulk liquid packaging storage, supporting up to 5 tons per bay with heavy-duty guide rails.
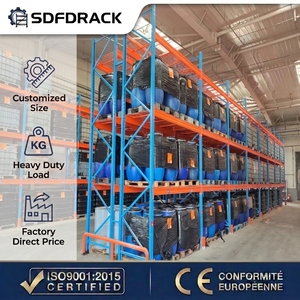
Engineered with integrated spill containment options, drum chocks, and chemical-neutral finish for hazardous liquid storage.

Flexible 3 to 6-tier modular stackable drum racks designed for compact footprint warehouse operations and export container loading.
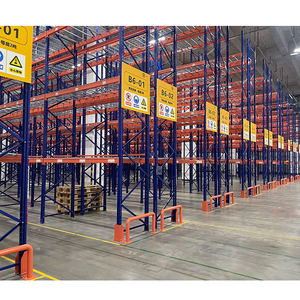
Direct factory customization offering cold-rolled Q235B/Q355B steel structural profiles, engineered CAD design, and full site compliance.
Storing liquid chemical raw materials, lubricants, solvents, and fuel oil drums presents distinct structural and environmental safety challenges compared to conventional unit-load palletized cargo. Cylindrical steel and high-density polyethylene (HDPE) 55-gallon drums concentrate heavy concentrated loads along narrow line contacts. When racked horizontally or vertically, these loads exert severe dynamic point loads, lateral rolling forces, and localized shear stresses on storage racking frameworks.
As leading China top drum storage pallet racking manufacturers & suppliers, our structural engineering team builds systems using high-tensile Q235B and Q355B cold-rolled structural steel. We integrate structural calculations designed to withstand extreme dynamic loading, high seismic risk factors, and aggressive chemical exposure. By incorporating custom drum cradles, integrated secondary spill containment sumps, and rigid beam safety locks, our racking systems optimize cubic storage density while mitigating the risks of catastrophic containment breaches.
Vertical drum racking allows direct top-side access via overhead drum lifters or specialized forklift attachments, rendering it ideal for sealed storage of high-density batch production. Horizontal drum racking (cradle-supported) enables gravity dispensing and decanting direct from the rack, but demands reinforced horizontal beam stop-chocks and secondary spill containment sumps underneath each bay to satisfy EPA 40 CFR 264.175 and NFPA 30 regulations.
How automation, environmental compliance, and smart sensors are reshaping liquid material handling infrastructure.
Modern chemical warehouses are transitioning toward Automated Guided Vehicles (AGVs) and specialized robotic drum clamps. Future drum racking designs feature wider entry guides, optical sensor alignment targets, and reinforced low-profile base plates to facilitate autonomous precision placement without manual driver intervention.
Sourcing requirements for global chemical hubs increasingly specify integrated sensor arrays embedded within secondary containment sumps. Micro-sensors trigger automated shut-off systems, flash warning beacons, and update warehouse control software (WCS) instantly upon contact with liquid hydrocarbons or corrosive compounds.
Conventional solvent coatings are being replaced by high-durability electrostatic polyester powder coatings and VOC-free Hot-Dip Galvanizing (HDG according to ISO 1461 standards). These finishes offer over 1,000 hours of salt-spray resistance, protecting structural integrity against acidic vapor exposure and ambient humidity.
Procurement teams are shifting away from stationary floor sumps toward modular, rack-integrated spill containment basins with removable galvanized steel mesh floor grating. This allows facilities to scale storage capacity while keeping containment volume compliant with regional EPA regulations.
Top-tier B2B buyers now mandate FEA stress simulations before approving manufacturing POs. By subjecting virtual rack models to dynamic impact forces and simulated seismic ground motions, engineers optimize steel gauge thickness, reduce unnecessary weight, and ensure maximum safety margins.
Standard engineering benchmarks for industrial oil and chemical drum racking systems.
| Engineering Parameter | Standard Heavy-Duty Specification | High-Capacity / Chemical Grade Spec |
|---|---|---|
| Primary Steel Material | Q235B Cold Rolled Carbon Steel (Yield Strength ≥ 235 MPa) | Q355B Structural High-Yield Steel (Yield Strength ≥ 355 MPa) |
| Load Capacity Per Level | 1,000 kg – 2,000 kg (Uniformly Distributed Load) | 2,500 kg – 3,500+ kg (Heavy Concentrated Liquid Load) |
| Beam Profile & Deflection Limit | Box Beam Profile (80mm – 140mm height), Deflection ≤ L/200 | Structural Channel / Heavy Duty Step Beam, Deflection ≤ L/300 |
| Surface Finish & Thickness | Thermosetting Epoxy Powder Coating (70 – 90 microns) | Hot-Dip Galvanized (ISO 1461 standard, 80–100+ microns) |
| Safety Pin Mechanism | Spring-loaded mechanical beam locking pins (Zinc Plated) | Bolt-locked structural safety retainers with shear test validation |
| Safety Code Compliance | EN 15635, ANSI MH16.1, ISO 9001:2015 | NFPA 30 (Flammable Liquids), OSHA 29 CFR 1910.106, EPA 40 CFR 264 |
With more than 20 years of dedicated manufacturing experience in warehouse storage racking and material handling equipment, our factory delivers end-to-end reliability for international buyers, project contractors, and regional distributors. Overseas buyers consistently tell us their primary concerns are steel gauge variances, unverified load capacities, inconsistent powder coating, and damage during international container shipping. We designed our production flow to eliminate these risks at the source:
From raw cold-rolled coil steel slitting, continuous precision roll-forming, automated robotic punching, and laser welding to our proprietary automated powder coating line, every step is executed within our own facilities.
Our experienced structural engineering team translates your specific building dimensions, floor load limits, drum dimensions, and forklift specifications into detailed 2D CAD floor plans and 3D FEA structural analysis models.
Components are precision-bundled with protective corrugated cardboard corners, stretch wrapped, clear part-numbered labeled, and packed to maximize sea container volume—reducing ocean freight cost per storage level.
Clear, technical answers to common engineering, safety, and logistical questions from global procurement teams.
To provide an accurate structural proposal and CAD drawing, our engineering team requires: (1) Warehouse clear height, column grid spacing, and floor slab load specifications; (2) Drum specifications including drum material (steel vs. HDPE plastic), gross weight when filled, dimensions (standard 55-gallon or custom volume), and storage orientation (horizontal dispensing vs. vertical standing); (3) Required secondary containment sump volume; and (4) Forklift truck type, lift height, and minimum aisle turning radius.
Our hazardous chemical drum storage systems can be designed with integrated spill sumps placed beneath the lowest beam level or across multi-tier bays. Containment capacities are engineered to hold a minimum of 10% of the total volume of all liquid containers, or 100% of the volume of the largest single container, fully complying with EPA 40 CFR 264.175 and NFPA 30 code standards for flammable and combustible liquid storage.
Yes. We manufacture fully compatible replacement components and extension bays for standard international hole pitch profiles, including 50mm pitch, 75mm pitch, Redirack style, and North American Teardrop profiles. Simply submit photos, beam section measurements, and connector pin configurations to our engineering department for verification before placing production orders.
For standard indoor warehouse environments storing sealed oil or non-volatile liquids, our standard electrostatic epoxy powder coating (70–90µm thick) provides excellent durability and abrasion resistance. For outdoor facilities, high-humidity coastal zones, or warehouses handling aggressive acids and solvents, we strongly recommend Hot-Dip Galvanizing (HDG per ISO 1461 standard), which provides a thick zinc-alloy barrier against rust and chemical attack.
Our heavy-duty steel drum cradles feature contoured, curved contact saddles that distribute the cylindrical weight of 55-gallon drums evenly across structural cross-ties and longitudinal beams. Rather than allowing a single line of contact to create point-load deflections, the cradle disperses weight across a broader surface area while incorporating integrated anti-roll steel chocks to lock drums in place.
Every production batch undergoes raw steel tensile testing, ultrasonic weld inspection, powder coating thickness gauge verification, cross-hatch adhesion testing, and full-scale beam deflection testing under 1.5x load factor limits. Complete Quality Assurance (QA) inspection reports and mill material certificates (MTC) are issued with export shipping documentation.
We advise equipping drum racking systems with heavy-duty HDPE or structural steel upright frame protectors, heavy column corner guards, rack end frame barriers, backstop safety beams to prevent over-pushing, and wire mesh or steel decking panels. These accessories protect key load-bearing columns from forklift impact damage, directly addressing OSHA 29 CFR 1910 and EN 15635 rack safety guidance.
Standard production lead time is 15 to 25 days depending on total order tonnage and custom finish requirements. Components are flat-packed in steel-banded bundles optimized for 20ft GP or 40ft HQ shipping containers. Uprights and beams are interleaved with shock-absorbing spacers to prevent powder coat scratching and maximize freight density.
Contact our structural racking engineering team today to receive a free warehouse layout CAD design, dynamic load analysis calculations, and direct factory pricing quotes within 24 hours.