Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Explore our export-grade structural pallet racking, automated storage solutions, and heavy-duty protective accessories manufactured to rigorous EN 15512 and AS4084 standards.
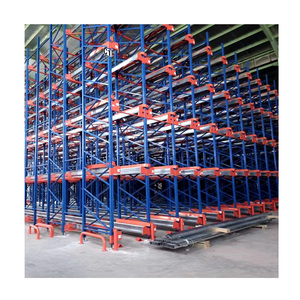
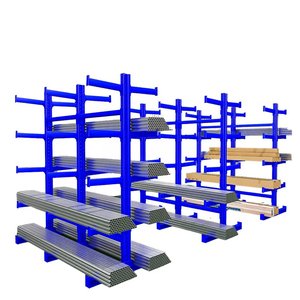
Modern logistics and high-density material handling demand structural stability, strict safety protocols, and optimized spatial throughput. As global supply chains scale up, warehouse infrastructure demands more than basic storage steel; it necessitates fully engineered, CE Certified Pallet Racking with Safety Barriers. Certified racking systems provide explicit structural safety margins under maximum dynamic load conditions, ensuring long-term operational continuity for distribution centers, third-party logistics (3PL) providers, and automated warehousing environments.
CE marking for industrial racking signifies strict compliance with European structural engineering guidelines, primarily EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design), EN 15629 (Specification of storage equipment), and EN 15635 (Application and maintenance of storage equipment). These standards govern cold-formed steel profiles, structural sway stability, bolt connection torque ratings, and frame deflection limits under full operational load capacities.
Key Technical Insight: Under EN 15635 guidelines, unshielded rack uprights situated at aisle intersections face an elevated risk of catastrophic structural collapse due to material handling equipment (MHE) collisions. Integrating heavy-duty steel safety barriers and HDPE column guards absorbs kinetic impact energy exceeding 1400 Joules, mitigating localized structural buckling and safeguarding operational personnel.
Selecting the ideal industrial pallet storage system requires evaluating inventory turnover, SKU depth, building clear height, and forklift turning radiuses. The following comparison highlights structural parameters across premier racking topologies:
| Racking Architecture | Selectivity (%) | Floor Space Utilization | Standard Load Capacity / Level | Recommended MHE / Forklift Type | Optimal Industry Application |
|---|---|---|---|---|---|
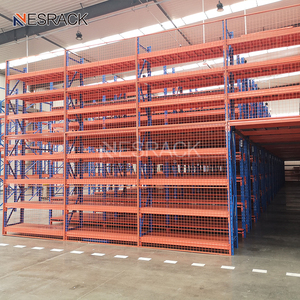
| Selective Pallet Racking | 100% Direct Access | 40% - 45% | 1,000 kg - 4,500 kg | Counterbalance, Reach Truck | High SKU variety, FMCG, Retail Fulfillment |
| Double Deep Racking | 50% Immediate | 55% - 60% | 1,000 kg - 3,000 kg | Deep Reach Truck, Pantograph Attachments | Cold Storage, Batch Production Logistics |
| Drive-In / Drive-Through | LIFO / FIFO Bulk | 65% - 75% | 1,000 kg - 2,000 kg | Specialized Narrow Counterbalance | Homogeneous bulk goods, Seasonal stock |
| Automated Radio Shuttle | Flexible LIFO / FIFO | 80% - 85% | 500 kg - 2,500 kg | Standard Forklift + Radio Shuttle Car | High-throughput distribution, Freezers (-30°C) |
| Cantilever Systems | 100% Long Loads | 50% - 65% | 500 kg - 6,000 kg per arm | Side Loader, Multi-directional Forklift | Pipes, Steel Profiles, Timber, Heavy Sheets |
Industrial safety barriers serve as the first line of defense against structural degradation in high-intensity logistical hubs. Material Handling Equipment (MHE)—such as reach trucks, electric stackers, and counterbalanced forklifts—frequently operate in narrow aisles where physical contact with racking uprights poses severe risks.
Fabricated from heavy-gauge structural steel (Q235B / Q355B) and finished in high-visibility safety yellow (RAL 1023) or hazard orange (RAL 2004), frame end protectors envelope the base of end-of-row upright frames. These barriers anchor directly into concrete slabs via chemical expansion anchors, shielding structural columns from corner-turning impact forces.
Upright column guards come in two primary forms: floor-anchored steel guards and clip-on High-Density Polyethylene (HDPE) wrap-around protectors. HDPE guards feature internal energy-absorbing air pockets that deform under impact and bounce back to shape, effectively absorbing localized shocks before permanent plastic deformation reaches the steel frame uprights.
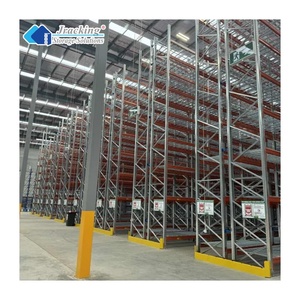
In Very Narrow Aisle (VNA) systems, structural ground-mounted guide rails ensure mechanical guiding of specialized MHE. These heavy-duty steel rails double as rigid safety barriers along the base of the entire aisle, preventing tracking deviation and preserving beam-column connector geometry.
The global storage equipment landscape is transitioning from static racking toward intelligent, automated, and environmentally sustainable structural systems. Procurement teams and engineering managers must factor the following technological trends into their long-term infrastructure investment plans:
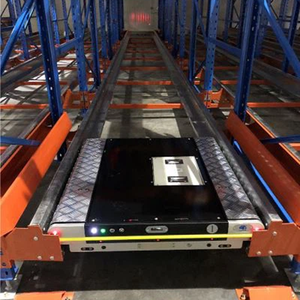
Semi-automated and fully automated pallet shuttle systems are replacing traditional high-density drive-in racking. Auto-shuttle technology eliminates forklift entry into racking aisles, dramatically reducing MHE impact damage. Modern CE-certified shuttle racking incorporates high-precision laser positioning channels, proximity sensors, and optimized structural steel rail tolerances to support continuous 24/7 AGV/AMR fleets.
Environmental durability is vital for cold storage, chemical processing, and outdoor logistics facilities. Industrial suppliers now provide advanced surface finishes tailored to ambient operational stresses:
The future of racking safety relies on IoT-enabled real-time monitoring. Structural strain gauges and vibration sensors embedded within safety barriers and load-bearing beams alert facility managers immediately when impact thresholds are exceeded or structural deflection limits (such as L/200) are breached. This proactive approach supports compliance with EN 15635 periodic inspection frameworks.
At Rack Pricing Storage Solutions Co., Ltd., we bring over two decades of OEM and ODM engineering experience to the global material handling market. Our integrated factory controls every phase of production—from raw coil processing to final container load planning.
In-house continuous roll forming lines, automatic punching matrixes, robotic welding stations, and continuous powder coating facilities guarantee precision tolerances across upright profiles and beam connectors.
Engineered and tested to meet international safety criteria, including European CE standards, EN 15512 structural codes, Australian AS4084 benchmarks, and OSHA 29 CFR 1910 guidance.
Our structural engineering team processes building floor plans, floor slab load constraints, pallet dimensions, and MHE specs to deliver complete 2D/3D CAD layouts and capacity calculations at no cost.
Components are part-numbered, bundled with protective cardboard film wrap at contact points, and loaded using optimized container space planning software to ensure undamaged transit and minimal freight cost per pallet position.
Comprehensive answers to critical technical, structural, and procurement inquiries submitted by international supply chain directors.