Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.
Explore our factory-engineered, high-capacity rack configurations certified to international safety and load performance standards.
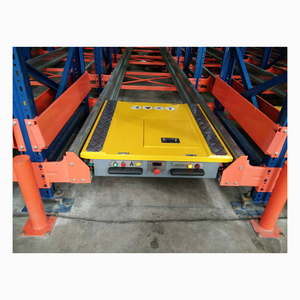
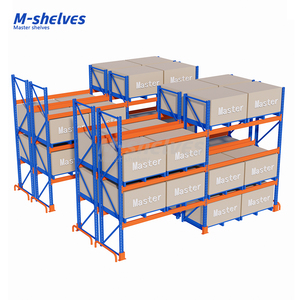
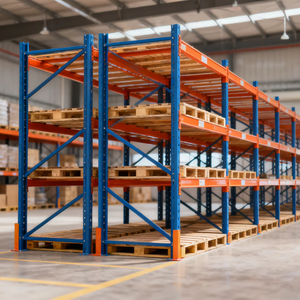
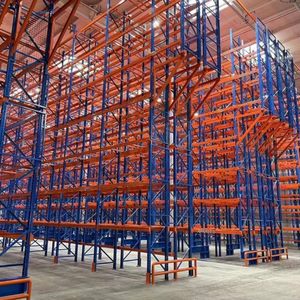
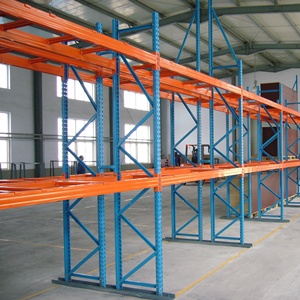
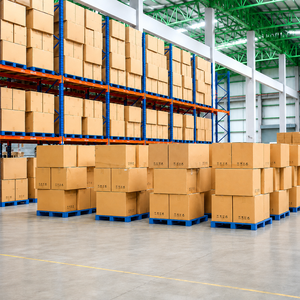
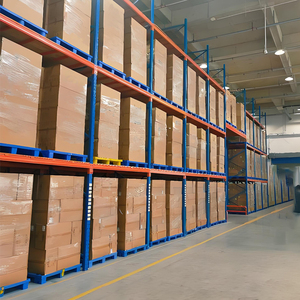
High rise pallet racking systems represent the structural backbone of modern automated logistics centers, cold storage facilities, and high-density distribution hubs. Operating at elevation thresholds ranging from 8 meters to over 30 meters, these systems demand rigorous engineering compliance to ensure structural integrity under dynamic seismic loads, asymmetrical pallet weight distribution, and high-frequency automated handling operations.
As a leading CE Certified High Rise Pallet Racking Manufacturer & Supplier, our structural engineering team utilizes high-grade cold-rolled structural steel (primarily Q235B and Q355B yield strength profiles) conforming to European Standard EN 15512 for structural steel racking design and FEM 10.2.02 codes. Compliance with CE EN 1090-1 execution standards guarantees that every upright frame, load-bearing cross beam, and diagonal bracing element undergoes non-destructive weld testing, precise dimensional tolerance checks, and strict yield stress analysis.
The structural resistance of high rise racking against lateral sway and frame buckling is directly proportional to profile geometry and material yield stress. Our specialized multi-stage cold-roll forming lines process continuous steel strips into upright columns featuring up to 13-fold deformation bending points. This complex geometric cross-section significantly elevates the moment of inertia ($I_x, I_y$) and section modulus, allowing vertical upright frames to absorb substantial axial loading without localized buckling.
| Racking Architecture Type | Maximum System Height | Typical Load Capacity / Level | Space Utilization Ratio | Compatible Material Handling Equipment |
|---|---|---|---|---|
| Selective High Rise Racking | Up to 12 Meters | 1,000 kg – 4,500 kg | 40% – 50% Floor Footprint | Standard Counterbalance, Reach Trucks |
| Very Narrow Aisle (VNA) Racking | Up to 18 Meters | 1,500 kg – 3,500 kg | 70% – 85% Floor Footprint | VNA Turret Trucks, Wire-Guided Pickers |
| Double Deep Pallet Racking | Up to 12 Meters | 1,200 kg – 3,000 kg | 60% – 65% Floor Footprint | Deep-Reach Telescopic Forklifts |
| Pallet Shuttle RGV Automated System | Up to 25+ Meters | 1,500 kg per Shuttle Bay | 85% – 92% High Density | Automated Rail Guided Vehicles (RGV) / AGV |
Engineered to fulfill strict international warehouse safety codes, optimizing vertical storage density without compromising operational safety.
Manufactured under strict ISO 9001 quality control and CE EN 1090-1 structural execution protocols. Factory-issued declarations of performance (DoP) ensure seamless compliance with EU build directives.
Maximizes clear building height up to 30 meters. Integrates with Narrow Aisle (VNA) and automated stacker cranes (AS/RS) to dramatically decrease cost per pallet position.
Thermosetting epoxy-polyester powder coating applied via automated electrostatic lines (60-80μm thickness) provides superior chemical resistance, impact protection, and extended service life.
As global supply chains transition toward smart warehousing and Industry 4.0 automation, the criteria for selecting high rise pallet racking suppliers have shifted beyond basic steel weight metrics. Procurement directors must evaluate compatibility with automated handling systems, long-term operational flexibility, carbon footprint emissions, and total cost of ownership (TCO).
Traditional forklift-reliant selective storage is rapidly giving way to dense, semi-automated and fully automated high rise racking layouts. Rail Guided Vehicles (RGV) and Autonomous Mobile Robots (AMR) require extreme manufacturing precision. Pitch tolerances along guide rails must stay within sub-millimeter thresholds ($\pm 0.5\text{mm}$) to prevent shuttle jamming and sensor misalignments during high-speed pallet retrieval.
High-rise racking structures installed in active seismic zones (such as earthquake-prone regions in North America, South America, and Asia-Pacific) require specialized ductile connection nodes and baseplate anchor assemblies. Modern procurement specifications increasingly mandate finite element analysis (FEA) dynamic simulations to verify structure response against cyclic seismic stress without catastrophic collapse.
Environmental, Social, and Governance (ESG) mandates are driving global buyers to favor high rise racking manufacturers utilizing scrap-recycled green steel and VOC-free powder coatings. Closed-loop chemical pretreatment systems minimize heavy metal wastewater discharge during production while ensuring optimal zinc-phosphate conversion coating for long-term corrosion prevention.
Our custom-designed racking profiles and heavy-duty shelving units are deployed across critical global supply chain sectors:
Specially formulated low-temperature powder coatings prevent micro-cracking at sub-zero conditions down to -30°C. High-density shuttle systems minimize refrigerated air volume loss.
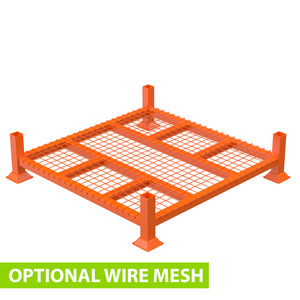
Heavy-duty multi-tier stackable post pallets and custom steel stillages engineered to handle heavy engines, stamping dies, and fragile body panels with 6-high stacking stability.
Integrated VNA racking with upper-level order picking platforms and wire mesh decking to maximize SKU density and speed up manual replenishment cycles.
Dust-free powder-coated surfaces, smooth weld seams, and anti-drop wire mesh decking engineered to maintain strict hygiene standards and protect packaged goods.
With over two decades of dedicated manufacturing experience, Rack Pricing Storage Solutions Co., Ltd. stands as an industry-trusted China pallet rack manufacturer and exporter. We deliver end-to-end material handling solutions directly from our production facilities to international importers, project contractors, 3PL providers, and equipment distributors worldwide.
We exercise total quality control over every manufacturing phase—from cold-roll profile forming, automated robotic welding, and shot blasting to automated powder coating and export bundling.
Our experienced structural engineering team provides complimentary warehouse layout planning, structural load calculations, and 3D CAD visualizations tailored to your specific forklift and pallet profile.
Equipped with an automated continuous thermosetting powder coating line capable of delivering customized RAL colors, anti-bacterial finishes, and heavy-duty outdoor galvanized surface options.
Components are systematically bundled, corner-protected, part-numbered, and securely strapped to maximize container cube utilization and eliminate transit damage during ocean freight.
Get clear, engineering-backed answers to essential procurement, structural safety, and custom manufacturing questions.
Partner with a verified CE certified high rise pallet racking manufacturer. Contact our engineering team for a complimentary warehouse CAD layout design, structural load analysis, and competitive direct factory quote.