Factory-direct warehouse racking & material handling equipment — 20+ years of manufacturing experience for global B2B buyers.

Verified OEM/ODM Factory Exporter

CE Certified Drive-Through Pallet Racking Manufacturer & Exporters

Engineered High-Density Warehouse Storage Solutions | Up to 85% Cubic Space Utilization | FEM 10.2.02 & EN 15512 Structural Compliance

Recommended Industrial Storage Systems

Precision-engineered, heavy-duty racking & logistical equipment certified for global enterprise distribution networks.

Custom Heavy Duty Industrial Steel Selective Pallet Rack Adjustable Warehouse Storage Rack Shelves
Wholesale Warehouse Racking Pallet Racks Industrial Selective Pallet Racking Heavy Duty Drive In Rack System
Warehouse Storage Rack Heavy Duty Pallet Racking with Safety Lock Pin for E-commerce Fulfillment Center
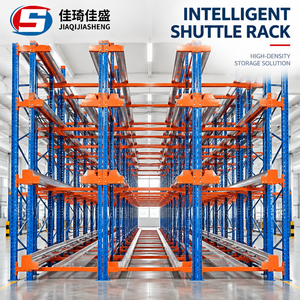
OEM ODM Customized Automation Upgrade High Space Utilization Intelligent Shuttle Rack for Manufacturing Plant
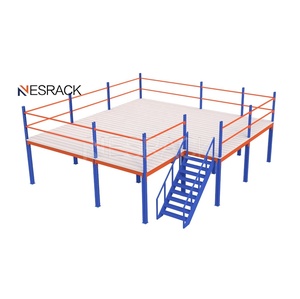
Heavy Duty Industrial Storage Warehouse Racks Pallet Racking Systems Attic Loft Mezzanine Floor Steel Platforms with Stair
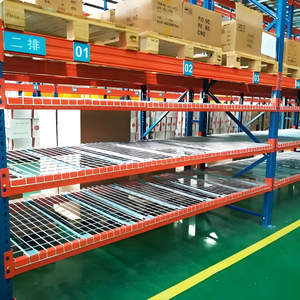
Heavy Duty Galvanized Wire Mesh Deck Pallet Rack Selective Racking System for Warehouse Industrial Storage Orange/Blue 3000mm
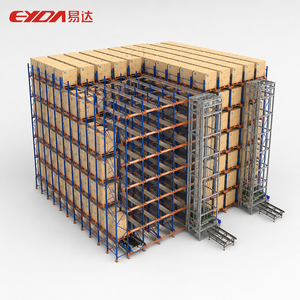
Heavy Duty Pallet Radio Shuttle Rack Automated Radio Shuttle Racking System For Food Beverage Warehouse
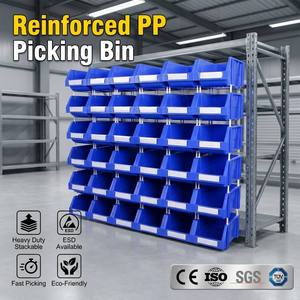
INORDER Semi-Open Stacking Warehouse Bin Spare Parts Picking Storage Organizer for Hardware Sorting Shelving Wholesale
20+
Years Manufacturing Excellence
85%
Max Space Utilization
100%
CE & ISO 9001 Compliant
50+
Global Export Countries

Engineering Excellence in Drive-Through Pallet Racking Systems

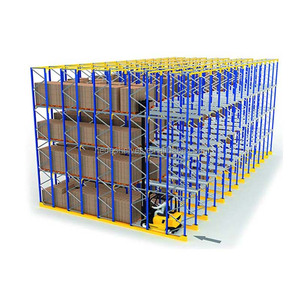
As a leading CE Certified Drive-Through Pallet Racking Manufacturer & Exporters, Rack Pricing Storage Solutions Co., Ltd. delivers high-density structural engineering optimized for fast-moving supply chains, cold storage facilities, and high-volume manufacturing hubs. Unlike traditional selective pallet racking that requires multiple operation aisles, drive-through racking eliminates work aisles to consolidate storage footprint, driving space efficiency upwards of 75% to 85%.

Understanding the distinction between Drive-In and Drive-Through racking is critical for industrial procurement directors. While Drive-In racking operates on a Last-In, First-Out (LIFO) inventory rotation with a single entry/exit point, Drive-Through Pallet Racking features dual access points (entry on one side, exit on the opposite side). This layout facilitates continuous First-In, First-Out (FIFO) stock management—making it the definitive engineering choice for date-sensitive food and beverage inventory, pharmaceutical storage, and high-throughput FMCG fulfillment centers.

Structural Anatomy & Technical Specifications

Our drive-through rack architecture relies on custom-rolled high-tensile structural steel profiles (grade Q235B and Q355B). Because forklifts navigate directly inside the racking lanes, structural stability and deflection control under load are engineered to rigorous EN 15512, FEM 10.2.02, and ANSI/RMI MH16.1 standards.

Engineering Parameter Standard Specification Custom Heavy-Duty Option
Steel Grade Selection Cold-Rolled Q235B High-Yield Steel Structural Q355B / S355 Micro-Alloy Steel
Pallet Load Capacity 500 kg to 1,500 kg per position Up to 2,500 kg per pallet position
Height Capability Up to 9,000 mm clear height Custom structural framing up to 13,000 mm
Surface Finish Electrostatic Epoxy-Polyester Powder Coating Hot-Dip Galvanized (HDG) for Cold Storage (-30°C)
Safety Protections Heavy-Duty Floor Guide Rails (83mm to 100mm) HDPE Column Protectors & Portal Top Frame Bracing

Each system is equipped with continuous heavy-duty cantilever support arms and stamped steel pallet runner channels. Designed with a tapered entry guide, these rails assist forklift operators in positioning pallets smoothly, mitigating impact wear and maintaining structural alignment even under continuous multi-shift operations.

Why Partner With Our Factory?

In-house manufacturing, certified steel processing, and turnkey layout design under one roof.

20+ Years Direct Manufacturing

We own fully automated roll-forming mills, CNC punching machines, and robotic welding lines, removing middleman markups and enforcing tight physical tolerances.

CE & International Certification

Our drive-through pallet racking systems strictly comply with European CE safety standards, ISO 9001 quality management, and international warehouse safety codes.

In-House Automated Powder Coating

Our dual automated electrostatic powder coating lines deliver uniform 70–90 micron finish thickness, ensuring superior scratch, impact, and corrosion resistance.

Free Engineering CAD Layouts

Our dedicated structural engineering team provides free 2D/3D CAD layout planning, aisle clearance optimization, and static seismic calculation reports before production.

Export-Optimized Logistics Packing

Components are precision-bundled with structural steel strapping, padded contact guards, and clear SKU labeling to optimize container space and simplify site installation.

Future Procurement Trends in Industrial Storage (2026–2030)

As global supply chains adapt to macroeconomic pressures, land costs, and labor shortages, procurement strategies for warehouse infrastructure are undergoing a paradigm shift. B2B buyers and logistics contractors are no longer sourcing storage racks as passive steel frameworks, but as integral components of integrated fulfillment engines.

1. Automated AGV & AMR Integration within Drive-Through Systems

Traditional drive-through racking required human forklift operators to enter narrow storage lanes. The future of high-density storage relies on Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs) equipped with LiDAR positioning. Modern drive-through rack procurement specs now require floor guide rails with embedded magnetic strips or laser reflectors, allowing autonomous lifts to navigate 1,400mm lanes with millimeter accuracy, virtually eliminating forklift collision damage.

2. Transition to Cold-Chain High-Density Footprints

With global demand for fresh food, biological products, and deep-frozen pharmaceuticals rising rapidly, cold storage operational costs are soaring due to high energy consumption. Modern warehouse procurement prioritizes drive-through and automated radio-shuttle systems that compress cubic cold-room space, reducing thermal loss and electricity overhead by up to 35% compared to wide-aisle selective racking.

3. Carbon-Neutral Manufacturing & Circular Steel Sourcing

Multinational corporations are enforcing stringent ESG (Environmental, Social, and Governance) compliance across their vendor supply base. Future procurement contracts heavily weight manufacturers who utilize recycled steel billets, eco-friendly degreasing chemistry, and zero-VOC powder coatings powered by solar-assisted manufacturing plants.

Technological Innovations Shaping Modern Racking Architecture

Driven by advancements in material science and structural engineering, high-density storage solutions are becoming stronger, safer, and infinitely more adaptable.

  • Ultra-High-Tensile Cold-Formed Steel Profiles: By transitioning from standard Q235 steel to micro-alloyed Q355B cold-rolled steel, upright frame wall thickness can be reduced while simultaneously increasing structural axial load capacity. This lowers overall shipping weight per container without sacrificing rack stability.
  • Modular Hybrid Drive-Through / Radio Shuttle Configurations: Modern logistics hubs are adopting hybrid configurations where drive-through steel frameworks are fitted with automated radio shuttle carts. This allows operators to seamlessly switch between manual forklift loading and fully automated channel retrieval as inventory volume scales.
  • Digital Twin & IoT Structural Health Monitoring: Next-generation enterprise installations integrate wireless strain gauges and piezoelectric shock sensors into critical rack upright legs. These sensors transmit real-time deflection and impact data to warehouse management software (WMS), alerting facility managers to structural damage before catastrophic frame failure occurs.
Frequently Asked Questions (Procurement FAQ)

Technical clarity for project managers, structural engineers, and international sourcing teams.

What information is required to design a customized CE Certified Drive-Through Racking System?

To produce an accurate engineering design and structural quote, our technical team requires:

  • Building floor plan dimensions, column placement, and clear overhead height under roof trusses/sprinklers.
  • Pallet specifications: Width, Depth, Height (including goods), and Maximum Gross Load Weight.
  • Forklift details: Outer overall mast width, maximum lifting height, turning radius, and minimum aisle entry clearance.
  • Environmental factors: Storage temperature range (ambient vs cold storage) and local seismic load requirements.
How does a Drive-Through Racking system differ structurally from Drive-In Racking?

While both systems utilize continuous horizontal pallet support rails and internal forklift access lanes, structural differences lie in their access profile. Drive-In Racking has a single entry/exit face and relies on heavy back bracing to maintain rigidity under load. Drive-Through Racking is open at both ends to allow FIFO inventory flow. Because it lacks single-face back bracing, drive-through systems utilize specialized top portal beam bracing and heavy-duty ground guide rails to guarantee frame stability.

What surface treatment is recommended for humid or sub-zero cold storage environments?

For standard ambient warehouses, our architectural-grade electrostatic epoxy-polyester powder coating delivers exceptional durability and chemical resistance. However, for sub-zero cold storage rooms (-20°C to -30°C) or highly humid processing facilities, we strongly recommend Hot-Dip Galvanizing (HDG) in accordance with ISO 1461. Hot-dip galvanizing seals both interior and exterior surfaces of steel tubing with a zinc layer, preventing internal rust formation for over 25 years.

Are your rack designs compliant with international safety standards like EN 15635 and OSHA?

Yes. All structural designs calculated by Rack Pricing engineers strictly observe European guidelines (EN 15512 / EN 15635), American RMI codes (ANSI MH16.1), and Australian standard AS 4084. We supply complete structural calculation documentation, maximum safety load notice plaques, safety lock pins, and impact protections to ensure full compliance during local municipal building inspections.

How do you optimize export packaging to prevent transit damage during ocean shipping?

Export components are packed with steel-banded structural bundles, corner cardboard guards, and waterproof plastic film wrapping. Small accessories (safety pins, footplates, anchors, bolts) are packed in heavy-duty wooden cases or steel crate bins labeled by part number. Our loading technicians calculate container volume using 3D stacking software to maximize payload efficiency, reducing freight costs per pallet position.

Request a Free Layout Design & Factory Price Quote

Transform your warehouse footprint with high-density CE certified racking engineered to your exact operational parameters. Speak directly with our engineering sales team today.